

Does Anyone Have Experience Drilling Holes in Square Tube?
Leave a message
I. Manual drilling
Manual drilling is a traditional drilling method. Its biggest advantages are low cost, simple operation, and wide application range.
1. Preparation
It is necessary to prepare square tubes, drill bits, screw drills, and other tools, and fasten the square tubes to the vise to prevent the square tubes from shaking during drilling.
2. Determine the drilling position
Use a ruler or ruler to measure and mark where the holes need to be drilled to ensure accurate positioning.
3. Start drilling
Use the screw drill to rotate clockwise at the location where the holes need to be drilled to gradually expand the hole diameter until the required size is reached.
4. Precautions
When drilling manually, pay attention to the following points:
(1) Use a drill bit with appropriate hardness and size;
(2) Maintain a constant speed and pressure when drilling;
(3) Do a good job of cleaning to prevent broken metal chips from harming the human body and equipment.
II. Machine drilling
Machine drilling is an efficient and accurate method suitable for occasions with large output and high precision requirements.
1. Preparation
Drilling equipment is required for machine drilling. CNC punching machines, integrated cutting machines, laser cutting machines, and other mechanical equipment are recommended.
2. Determine the drilling position
Use computer drawing software or manual marking to determine the location, hole diameter, hole spacing and other parameters to be drilled.
3. Start drilling
Use the equipment to perform drilling operations. You can complete drilling multiple holes at one time according to the preset parameters.
4. Precautions
The following points should be noted when drilling with a machine:
(1) The equipment needs to adjust the appropriate processing parameters and tools;
(2) Ensure the safety of the equipment and operators when drilling;
(3) The equipment needs regular maintenance to ensure normal operation.
In summary, manual drilling is suitable for small batches of simple hole diameters, and machine drilling is suitable for large batches of complex hole diameters. When using, it is necessary to select the most suitable drilling method based on the actual situation to ensure work efficiency and quality.
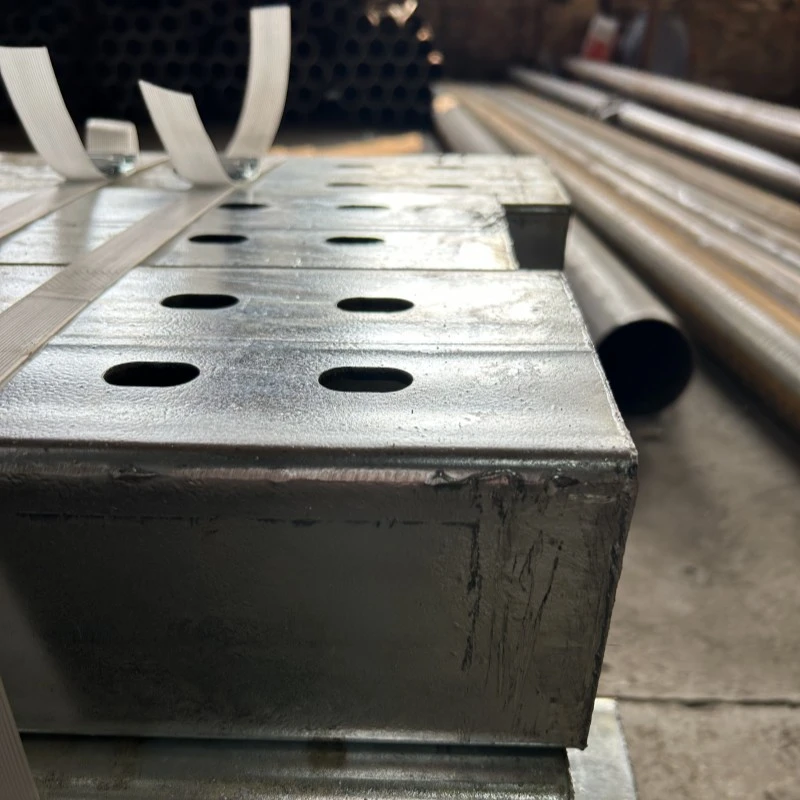
One thing that needs to be noted is how to prevent defects in the punching of thick-walled square tubes
Many defects of square tubes are caused during punching, so the power transfer process of square tube blanks is the key procedure for producing square tubes. The main difficulty of high alloy perforation is the low perforation performance. For the sake of quality, the deformation parameters of perforation should be rationally selected. Small compression will cause instability in the perforation process. Therefore, when the critical compression is small, the plug should be set at about 7% of the front compression, otherwise it will not bite, and even move more or get stuck in the front. The increase in compression in front of the plug will also form a cavity and sink the defects inside. Therefore, if you want to overcome the problem, the tube blank must be centered, and the centering hollow depth should be compared with other steel grades.
Therefore, the heating system is the temperature of the outlet and the requirements for heating quality. The quality of heating depends to a large extent on the heating operation and heating system. A relatively small value of the ellipticity coefficient is generally beneficial to improve the quality of the rough tube and limit the transverse deformation. However, it is not good if the ellipticity coefficient is too small, which will cause difficulties in rotating the rolled piece and even cause wear of the guide plate, which is easy to cause defects on the surface.
When perforating square tubes, the wear of the guide plate should be generally checked. Once found, it should be replaced immediately. The degree of ellipse should be controlled in the range of 1.07-1.08. The key process of heating the square tube billet also affects the normal progress of the subsequent processes, which also has a great impact on the quality of the finished product.


